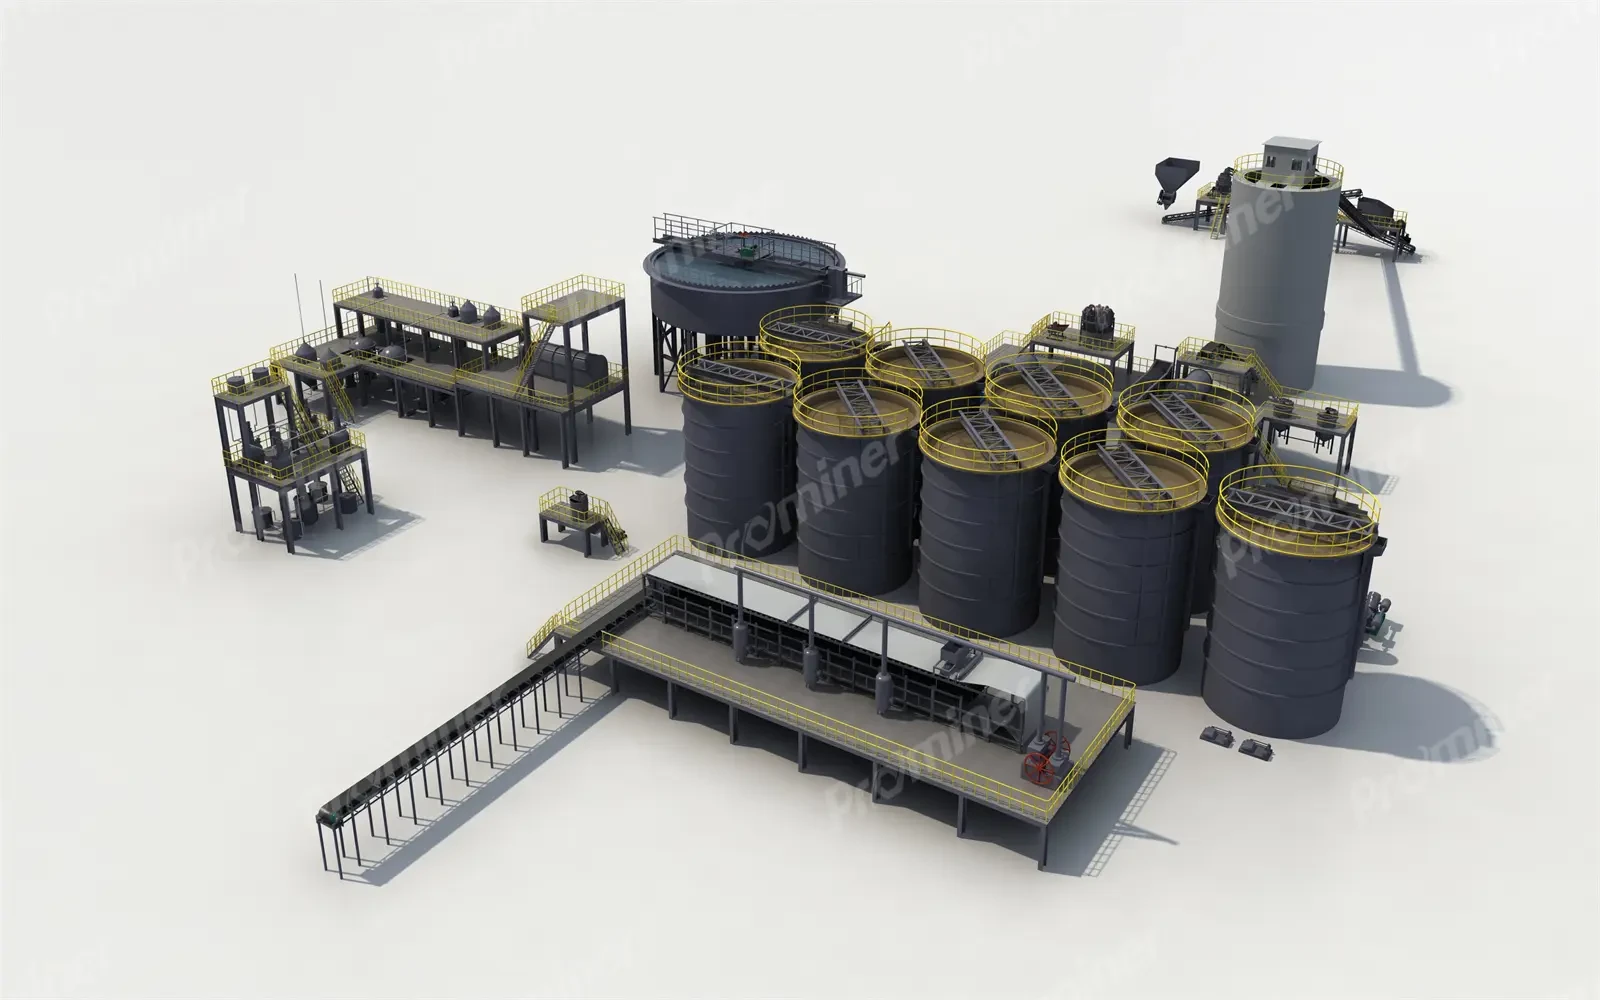
How a CIP or CIL Gold Plant Works
A CIP or CIL plant recovers gold that is too fine for gravity. Ore is milled to a fine slurry, gold is dissolved with dilute sodium cyanide in a train of agitated tanks, and the dissolved gold is captured on granules of activated carbon. The loaded carbon is then stripped in an elution and electrowinning plant.
CIL (carbon in leach) puts carbon in every tank, so gold is adsorbed as soon as it dissolves. CIP (carbon in pulp) leaches first, then adsorbs in a separate set of tanks. For the full comparison, including recovery, capital cost, preg-robbing ore and heap leach, see the difference between CIP and CIL.
A complete circuit, from ore to gold, includes:
- Crushing and milling to about 80% passing 75–150 µm, with a centrifugal concentrator in the mill circuit to take out coarse gold first.
- Thickening to 40–50% solids, which sets tank volume and cyanide use.
- Leach and adsorption tanks, 5–8 agitated tanks in series, with lime for pH 10.5–11.5 and air or oxygen for 6–10 ppm dissolved oxygen.
- Interstage screens that keep carbon in each tank while slurry flows on.
- Carbon transfer, pumping carbon upstream against the slurry so the richest carbon meets the richest solution.
- Elution, electrowinning and regeneration to recover gold and reactivate the carbon.
- Cyanide detoxification and a lined tailings storage facility.
CIP Plant Design: The Numbers That Size the Plant
Every CIP or CIL plant design is built on a few parameters. All of them should come from test work on your ore (see test work before you buy a plant), not from a catalogue.
| Parameter | Typical range | What it decides |
|---|---|---|
| Grind size | 80% passing 75–150 µm | Gold liberation and recovery; mill power |
| Leach residence time | 18–36 h total | Total tank volume |
| Slurry density | 40–50% solids | Slurry volume per tonne; agitation power |
| Cyanide | 150–500 ppm NaCN | Leach rate and reagent cost |
| pH | 10.5–11.5 (lime) | Cyanide stability; keeps HCN gas from forming |
| Dissolved oxygen | 6–10 ppm | Leach rate; air or oxygen supply |
| Carbon concentration | 10–25 g/L of pulp | Adsorption rate and carbon inventory |
| Number of tanks | 5–8 | Carbon staging and short-circuiting risk |
| Interstage screen aperture | 0.6–0.8 mm | Carbon retention; must pass slurry, hold carbon |
Sizing the tank train: a worked example
Working volume = slurry volume per hour × residence time. The planning example adds 10% of working volume; actual freeboard is a separate design decision. Slurry volume per day is the ore volume (tonnes ÷ ore density) plus the water carried at the target solids density. The table assumes ore density 2.7 t/m³, 45% solids, 24 hours residence, water density 1 t/m³, an illustrative 10% addition to working volume for freeboard planning, and six equal tanks:
| Plant throughput | Total tank volume | Six tanks of about |
|---|---|---|
| 50 t/day | ≈ 88 m³ | 14.6 m³ each |
| 100 t/day | ≈ 175 m³ | 29.2 m³ each |
| 250 t/day | ≈ 438 m³ | 73.0 m³ each |
| 500 t/day | ≈ 876 m³ | 146.0 m³ each |
Double the residence time and the volume doubles; run at 40% solids instead of 45% and it rises by about 17%. Carbon advanced from the train each day sets the elution batch. See sizing the carbon batch. For a small-plant view of the same calculation, including consumables per tonne, read the small CIP and CIL plant guide.
Gold CIP Tank Maintenance: What Fails and How to Catch It
The maintenance schedule further down the page gives routine intervals. This section covers the failures that quietly cost recovery in a CIP or CIL tank train, and the check that catches each one early.
| Failure | Symptom | Check |
|---|---|---|
| Interstage screen blinding | Tank level rising, slurry overflowing the launder | Screen differential level every shift; clean or run the sweep/airlift |
| Worn or torn screen | Carbon found in downstream tanks or tailings; gold lost with fine carbon | Sieve a tailings sample for carbon daily; inspect wedge-wire panels |
| Carbon attrition | Carbon inventory falling; rising fine carbon in tailings | Weekly carbon inventory per tank; check agitator speed and transfer pump type |
| Low carbon activity | Solution gold rising in the last tanks at steady feed | Activity test on carbon samples; regeneration kiln performance |
| Agitator wear or failure | Sanding in the tank bottom, short-circuiting, lower recovery | Motor current trend, gearbox oil, impeller and shaft wear at shutdowns |
| Lime scaling | Scale on screens, pipes and carbon; slower elution | pH control stability; acid wash results on carbon |
| Low dissolved oxygen | Slower leach, gold left in tailings | DO meter per tank; air sparger and blower condition |
| Liner or shell corrosion | Leaks, weeping welds, stained plinths | Annual internal inspection; containment bund condition |
CIL & CIP Gold Plants Specifications
The figures below describe typical industry specifications for this class of equipment rather than a single fixed model. Use them to scope a requirement, then confirm exact figures against the supplied unit before purchase.
| Specification | Typical value |
|---|---|
| Typical recovery | 88–95% on free-milling ore |
| Total residence time | 18–36 h across the tank train |
| Number of tanks | 5–8 in series |
| Slurry density | 40–50% solids by mass |
| Grind size | 80% passing 75–150 µm |
| Cyanide concentration | 150–500 ppm NaCN |
| pH control | 10.5–11.5 with lime to suppress HCN |
| Dissolved oxygen | 6–10 ppm, air or oxygen sparged |
| Carbon concentration | 10–25 g/L in the pulp |
| Carbon activity | Regenerated on a kiln cycle to maintain loading |
| Interstage screening | Mechanical or airlift, 0.6–0.8 mm aperture |
| Throughput range | 50–2,000 t/day for modular plants |
CIL & CIP Gold Plants: Uses and Applications
- Free-milling hard-rock gold ore
- Oxide and transitional ore treatment
- Gravity tailings scavenging
- Central processing facilities serving multiple small miners
Maintenance Schedule
Most premature failures in this equipment class trace back to a missed routine check rather than a design fault. The intervals below are a practical starting schedule; adjust them to your duty cycle and the manufacturer manual.
| Interval | Task |
|---|---|
| Every shift | Check cyanide and pH in each tank; verify agitator operation and interstage screen flow; monitor dissolved oxygen. |
| Weekly | Carbon inventory and activity check; inspect screens for blinding and carbon bypass. |
| Monthly | Agitator gearbox oil and impeller wear inspection; tank liner and launder condition check. |
| Quarterly | Carbon regeneration kiln service; pump and pipework wear survey. |
| Annually | Tank internal inspection and relining as needed; full cyanide management review against the International Cyanide Management Code. |
Frequently Asked Questions
What is a CIP plant?
A CIP (carbon-in-pulp) plant is a gold processing plant that dissolves gold from finely milled ore with dilute cyanide in agitated tanks, then captures the dissolved gold on activated carbon in a following set of tanks. The loaded carbon is stripped in an elution plant and the gold is recovered by electrowinning and smelting.
What does CIL mean in gold processing?
CIL stands for carbon-in-leach. Activated carbon is added to the leach tanks themselves, so gold is dissolved by cyanide and adsorbed onto carbon in the same tanks at the same time. It uses fewer tanks than CIP and is the usual choice for small and medium plants.
What is the difference between CIL and CIP?
In CIL, leaching and carbon adsorption happen simultaneously in the same tanks. In CIP, the ore is leached to completion first and carbon adsorption happens in a following train. CIL uses fewer tanks and lower capital cost and suits ore with preg-robbing carbonaceous material; CIP gives cleaner control of each step and slightly better carbon management.
What recovery should a CIL plant achieve?
88–95% on free-milling ore. Refractory ore where gold is locked in sulphides or associated with carbon can drop well below that without pre-treatment such as flotation, roasting or pressure oxidation. Diagnostic leach test work before plant design is essential, not optional.
Is cyanide use legal for gold processing in Tanzania?
Yes, under permit and subject to environmental regulation administered by NEMC and the Mining Commission, with requirements covering storage, tailings containment, monitoring and emergency response. Many operators additionally align with the International Cyanide Management Code. Obtain current legal advice and permits before procuring a plant.
How fine must ore be ground for CIL?
Typically 80% passing 75–150 µm. Finer grinding liberates more gold and lifts recovery, but grinding energy rises steeply and is usually the largest single operating cost. The economic grind size is determined by test work balancing recovery gain against milling cost.
What size CIL plant makes economic sense?
Modular plants from about 50 t/day are commercially available and are commonly used by small to medium Tanzanian operators, sometimes as shared central processing facilities. Below roughly 20–30 t/day, gravity recovery alone is usually the better economic answer.
Supply and Delivery Across Tanzania
Bart Mining supplies cil & cip gold plants and related equipment to mining operations throughout Tanzania, with primary coverage of the Lake Victoria Goldfields (Mwanza, Kahama, Geita, Shinyanga and Bukombe), alongside the Lupa Goldfields around Chunya and Mbeya, and delivery nationwide from Dar es Salaam.
Commonly supplied to: Dar es Salaam.
Manufacturer or supplier of this equipment? Bart Mining sells machinery like the cil & cip gold plants to buyers across Tanzania through its local market partnership.
Safety and scope references: Cyanide Code scope · Mining Commission licence services